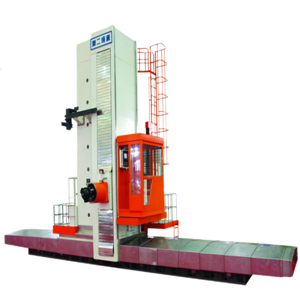
How a CNC Floor Type Milling And Boring 天美直播Improves Large-Part Production (2)
Why boring accuracy matters in large components
In many large mechanical parts, holes are not simply through holes.
They might be:
Bearing holes
Mounting holes
Shaft holes
Connection holes
Precision locating holes
Large-diameter holes
These holes often directly determine the final assembly quality.
For example, if the bearing holes on a large machine base are misaligned, assembly problems may occur when installing bearings, shafts, and other components.
Therefore, boring operation in the machining of large workpieces is not simply "machining holes".
What really matters is:
The location, size, coaxiality, and relationship of the hole with other machining references.
This is why many large manufacturing companies choose to integrate milling and boring into the same type of equipment.
By using a unified clamping system, multiple key machining steps can be completed within the same machining coordinate system.
Combining milling and boring for process integration
The traditional processing flow may be:
Milling 天美直播→ Inspection → Workpiece Transfer → Boring 天美直播→ Inspection → Secondary Milling
With the use of Floor Type Milling and Boring Machine, some workpieces can be processed using a more centralized workflow:
Workpiece Setup → Rough Milling → Face Milling → Drilling → Boring → Reaming → Finishing
Of course, the actual process still needs to be determined based on the workpiece structure, material, size, and precision requirements.
However, the core change in the processing flow lies in:
More machining tasks can be completed around the same clamping datum.
For large workpieces, this change is often more meaningful than simply increasing the spindle speed.
Because the efficiency of large-scale production is not just:
Cutting Time
Instead:
Total Production Time = Setup + Handling + Cutting + Inspection + Rework
If equipment can reduce setup and handling, then even if the single-cut speed does not change significantly, the overall production cycle can still be improved.
High torque and stable cutting for heavy materials
Large industrial parts are typically not thin-walled, small parts.
Many applications require processing:
Cast iron
Carbon steel
Alloy steel
Structural steel
Other engineering metals
Different materials produce different cutting resistances.
Especially in the rough processing stage, a large amount of material needs to be removed quickly.
This requires the equipment to have sufficient spindle capacity and structural stability.
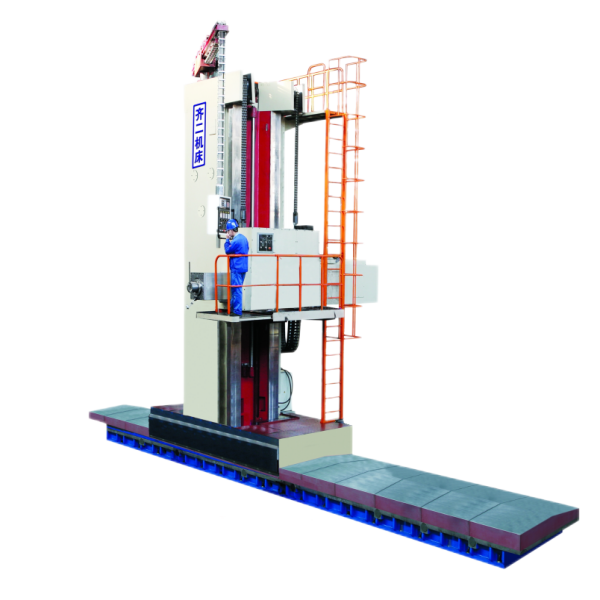
The Floor Type Milling and Boring Machine product system, emphasizing its high rigidity structure, high torque spindle, and multi-axis machining capabilities; some products also support machining operations such as drilling, reaming, boring, grooving, and end milling.
In actual production, the value of high torque is not to make the equipment "look stronger", but to make the equipment more suitable for heavy cutting conditions.
Especially during the rough machining of large workpieces, the equipment needs to remain stable under reasonable cutting parameters.
If the equipment experiences significant vibration, it may result in:
Tool wear increases
Surface quality decreases
Cutting parameters must be reduced
Production time increases
Tooling cost rises
Therefore, what heavy machining really needs is:
Power + Torque + Rigidity + Stability
Instead of pursuing a single parameter.